Submersible Pump Power Unit HPUSP Series / Technical Archive
For Pump Head Matching
Hydraulic Supply for Submersible Pump Heads

Hydraulic Power Unit for Submersible Pumps

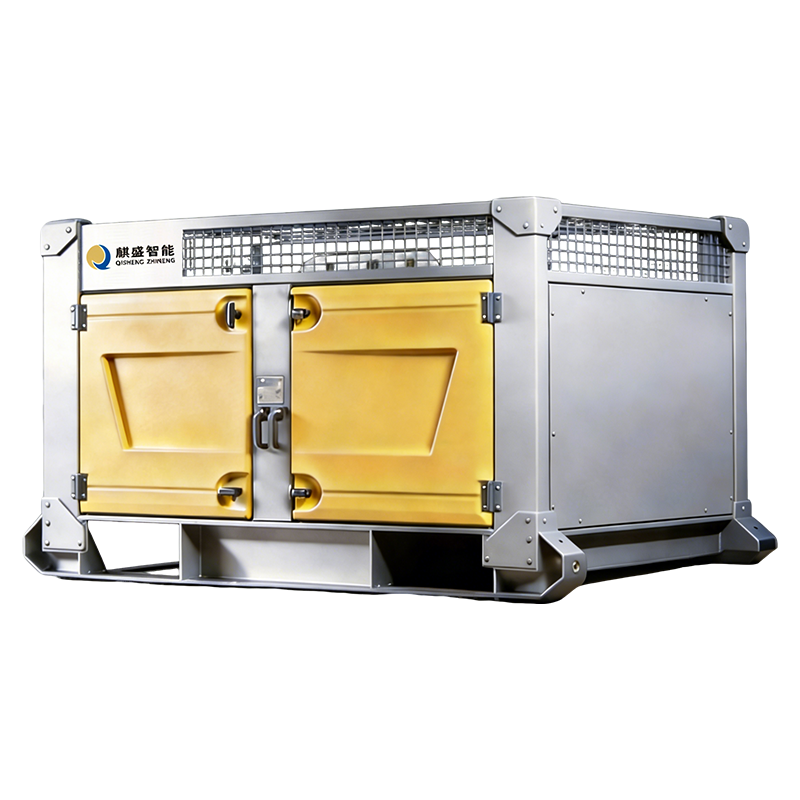
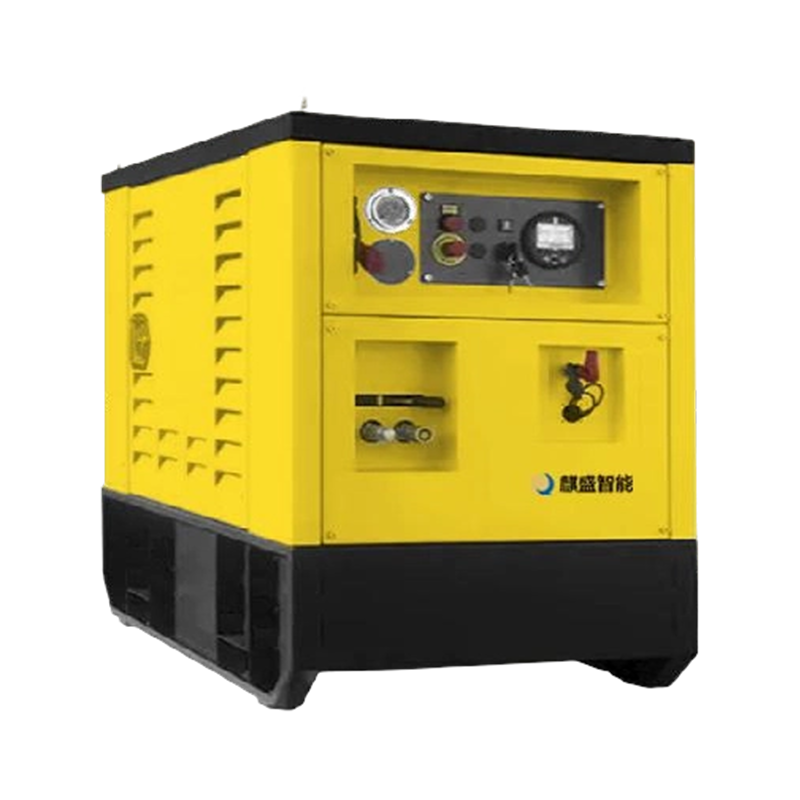
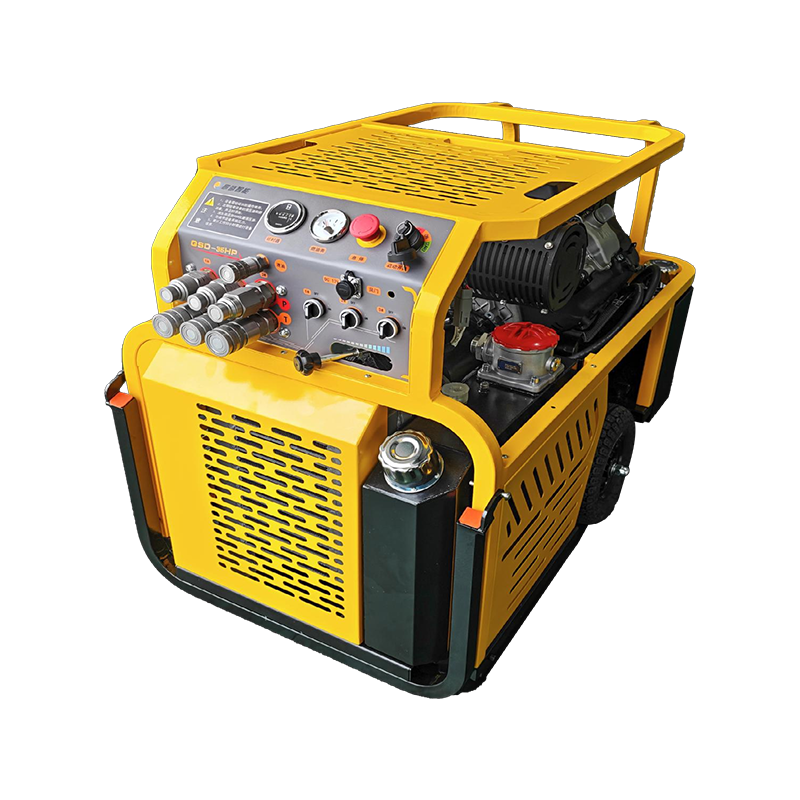
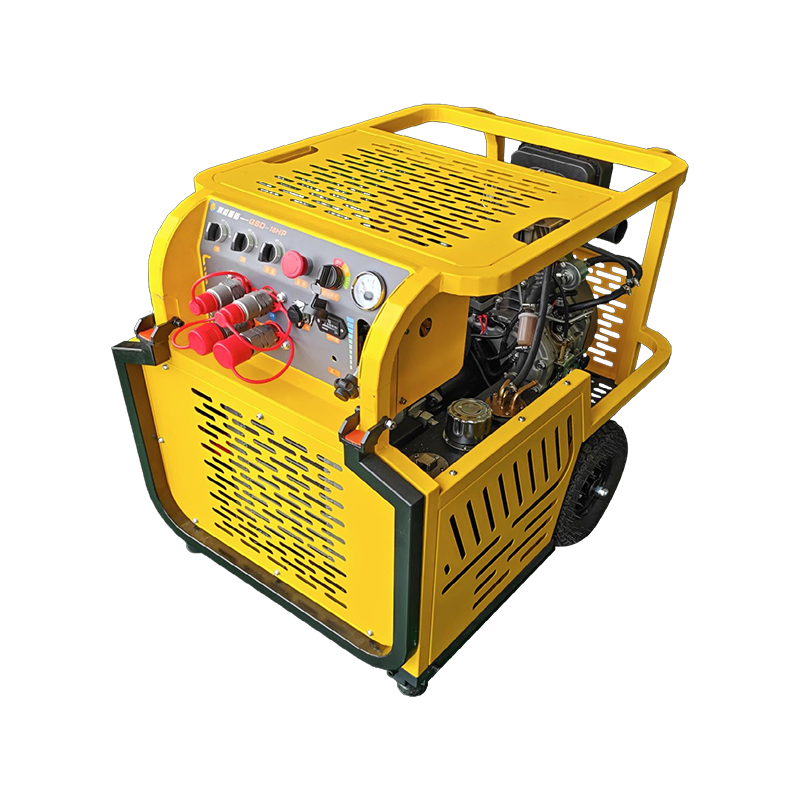
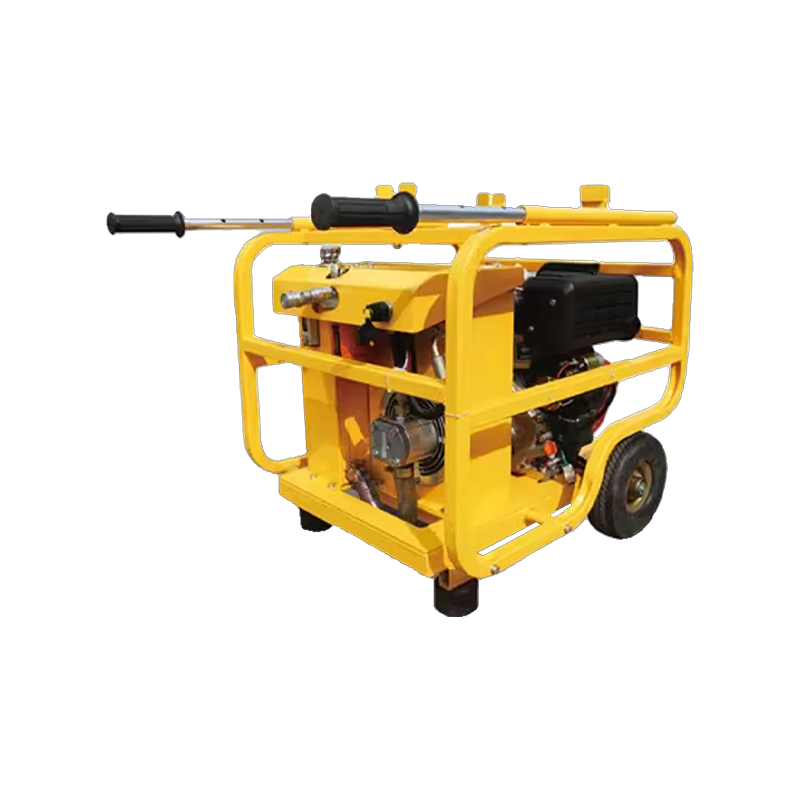
Engine-driven hydraulic power unit configured to supply hydraulically driven submersible pump heads, with matched flow, pressure, and coupler arrangements for sumps, chambers, and flood control duties

Power Unit Pump Head
35 L/min Rated Flow
210 bar Working Pressure
9.0 kW Engine Output
18 L Reservoir
IP68 Pump Head Rating
Unit Configuration
Unit type Engine-driven hydraulic power unit
Engine output 9.0 kW gasoline, air-cooled
Starting system Recoil with decompression
Rated flow 35 L/min
Working pressure 210 bar
Relief valve setting 230 bar, factory set
Reservoir capacity 18 L
Filtration rating 10 micron absolute, return line
Couplers Flat-face quick couplers, 2 sets
Fuel tank capacity 6.5 L
Runtime at rated load Approximately 3.2 hours
Handling Skid with lifting eyes and forklift pockets
Product Introduction

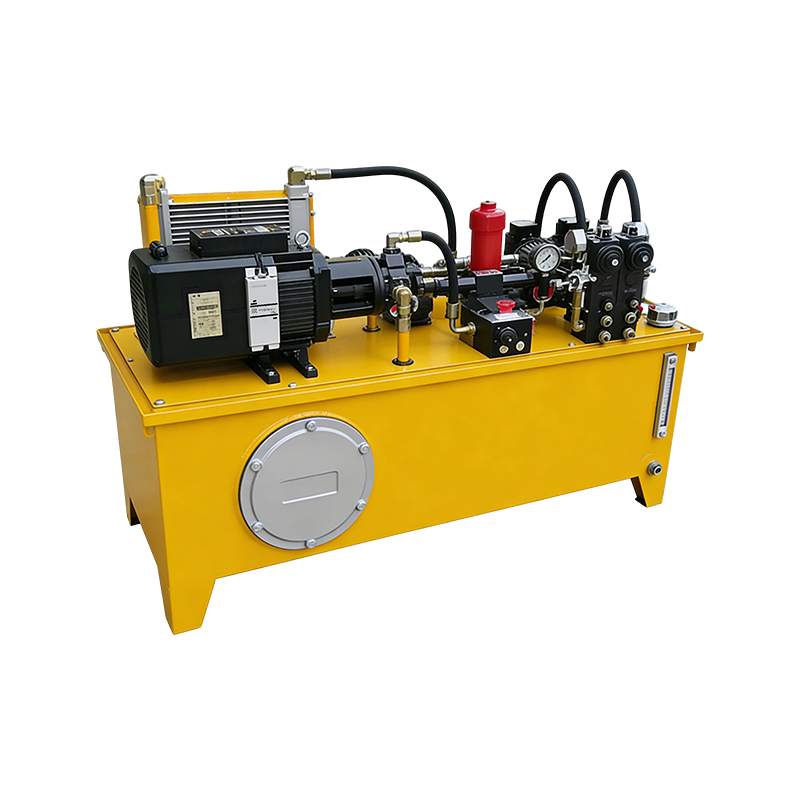
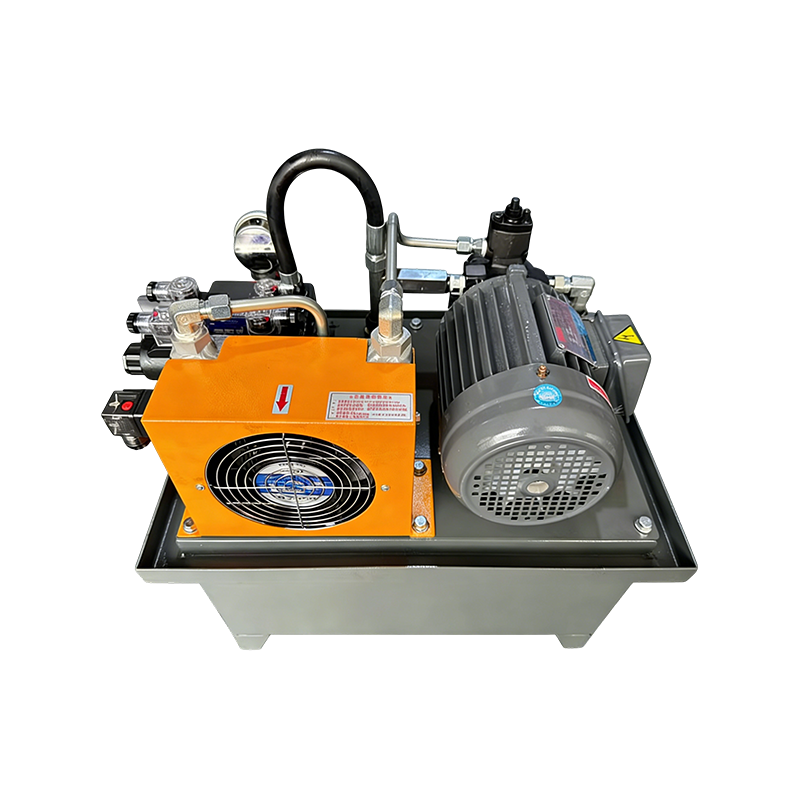
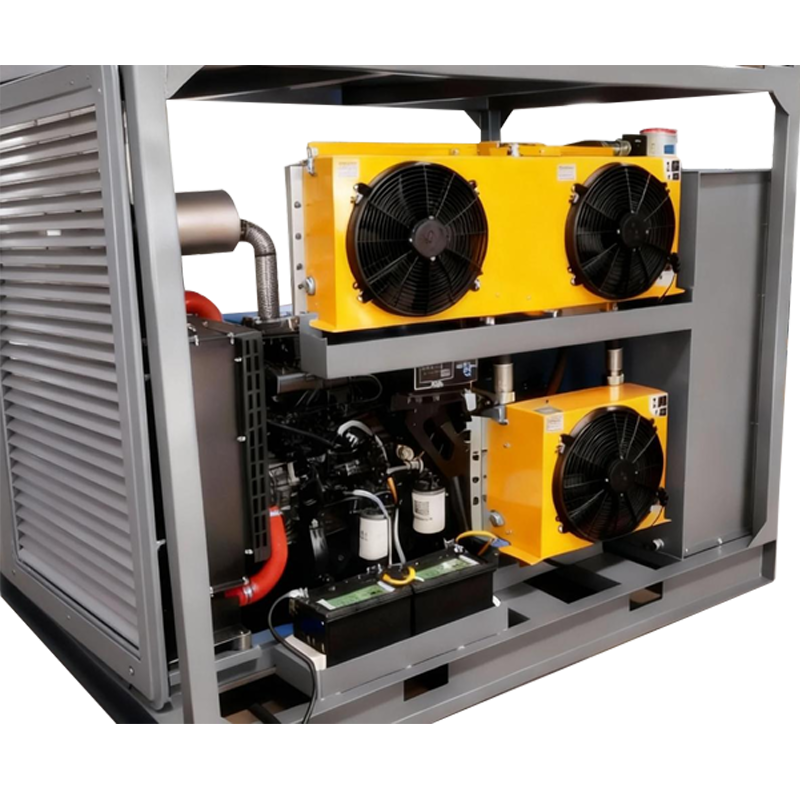
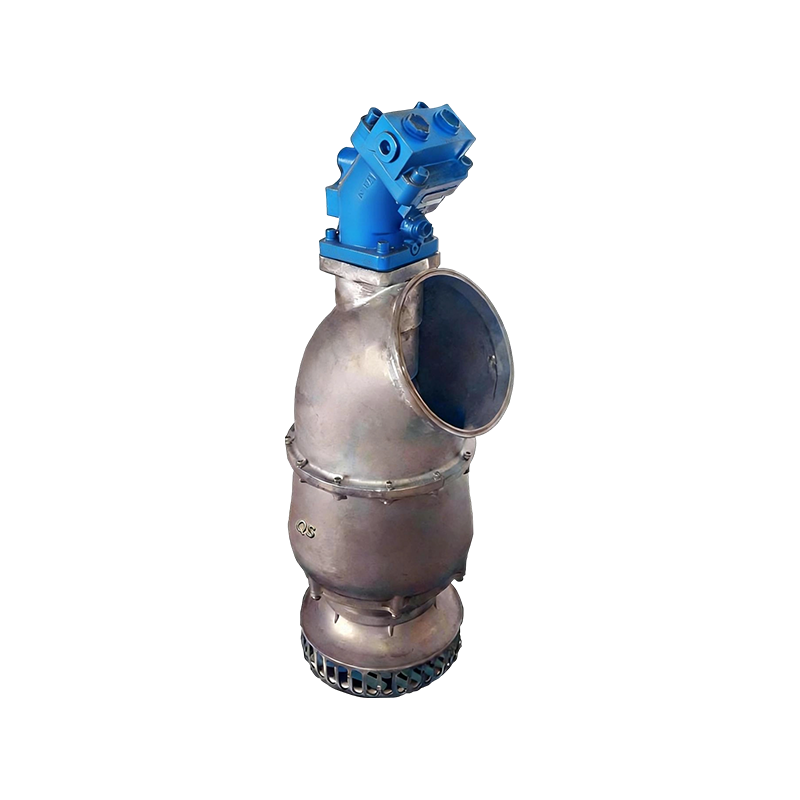
The Hydraulic Power Unit for Submersible Pumps is an engine-driven hydraulic power unit designed to supply hydraulically driven submersible pump heads used in drainage, dewatering, and flood control operations. The unit integrates a 9.0 kW air-cooled gasoline engine with a variable-displacement hydraulic pump rated at 35 L/min and 210 bar, an 18-litre reservoir with 10-micron filtration, and two sets of flat-face quick couplers. Because the submersible pump head contains no electrical motor or cable, the power unit can supply pumping in sumps, chambers, and flooded spaces where electrical equipment in wet conditions is restricted. The pressure-compensated pump adjusts displacement as pump head demand changes, supporting stable pumping as water levels and discharge conditions vary. The unit can drive one or more pump heads of matched hydraulic specification, subject to the combined flow demand. The unit is suited to procurement by drainage contractors, municipal maintenance departments, and rental operators maintaining a stock of hydraulic submersible pump heads.

Core Advantages
01
Matched Supply for Submersible Pump Heads The unit's flow and pressure are selected to match the hydraulic motor displacement of the submersible pump heads, so the correct impeller speed is achieved without field matching. Buyers should provide the pump head specification at inquiry stage so the pump displacement and relief setting can be confirmed.
02
No Electrical Equipment in the Water Power is transmitted hydraulically from the surface-mounted unit to the submerged pump head through hoses. No electrical motor, cable, or junction box is present in the water, which simplifies electrical safety management in sumps, chambers, and flooded areas.
03
Single Unit, Multiple Pump Heads One power unit can drive several submersible pump heads of matched specification, allowing coverage across multiple sumps or chambers. This reduces the number of power units required on a site, provided the combined flow demand of the connected heads does not exceed the unit's output.
04
Pressure-Compensated Output The variable-displacement pump adjusts displacement as pump head demand changes, reducing flow when the head operates against lower resistance. This limits heat generation and fuel consumption compared with fixed-displacement supply, and supports stable pumping as conditions vary.
05
Independent of Mains Electricity The gasoline engine drives the hydraulic pump directly, so pumping can continue where electrical supply is unavailable, damaged, or restricted. This suits flood response, remote sites, and construction dewatering without temporary power.
06
Skid Mount with Handling Provisions The steel skid includes lifting eyes and forklift pockets for mechanical handling, allowing the unit to be positioned by crane or forklift at the water source. Component mounting and frame construction are specified for sustained pumping duty.
Submersible Pump Head Compatibility
General Drainage Pump Heads Hydraulically driven submersible pump heads for sump, chamber, and pit drainage. The 35 L/min flow supports impeller speeds matched to the pump head specification.
Trash and Solids-Handling Heads Pump heads with semi-open impellers for water containing debris. Higher torque demand during solids passage is met by the pressure-compensated supply.
Slurry and Abrasive Service Heads Heavy-duty pump heads for high-density or abrasive water. Buyers should confirm the flow and pressure requirement of the head, as higher density increases hydraulic power demand.
High-Head Pump Heads Pump heads configured for elevated discharge points. The 210 bar working pressure supports higher head requirements within the pump head's rated capability.
Multi-Point Dewatering Arrangements Configurations where one power unit serves several pump heads at different sumps. A flow divider arrangement may be required, to be confirmed against the number of heads and their duty points.
Existing Fleet Pump Heads Operators with existing hydraulic submersible pump heads can specify the power unit to match their pump motor displacement and coupler type, extending the life of existing pump inventories.
Deployment Scenarios
D1
Construction Site Dewatering Power supply for submersible pump heads in excavation pits and foundation sumps. The engine-driven unit operates without temporary electrical supply on site.
D2
Municipal Sump and Chamber Pumping Power supply for pump heads used in sewer sumps, stormwater chambers, and maintenance holes. No electrical cable is routed into the wet chamber.
D3
Flood Response Operations Power supply for floodwater removal where electrical infrastructure is affected. The unit can be positioned at a safe distance from the flooded area with hoses running to the pump head.
D4
Multi-Sump Coverage One power unit serving several submersible pump heads at different sumps, reducing the number of power units required on a large site or along a drainage network.
D5
Remote and Off-Grid Sites Pumping at locations without electrical supply. The engine drive allows dewatering to proceed independently of grid power or generator availability.
D6
Fleet and Rental Stockholding Rental operators and drainage departments hold power units to drive a stock of hydraulic submersible pump heads, standardising the supply side while covering different pump head duties.
Manufacturing and Supply Capabilities
Engine and pump integration Engine and hydraulic pump coupled through a bell housing and flexible coupling, mounted on a common base. Alignment and run testing performed during assembly; tolerances and test records to be confirmed with the factory.
Pump head matching Hydraulic motor displacement and relief setting selected to match the submersible pump head specification, ensuring the correct impeller speed and stable operation. Matching confirmed against pump head data supplied at order stage.
Hydraulic circuit assembly Reservoir, filtration, relief valve, pressure gauge, and couplers assembled and pressure tested as a complete circuit. Circuit schematic and component list available with the unit.
Custom configuration Coupler type, hose length, relief valve setting, and pump displacement can be adjusted to match existing pump head inventories. Multi-head distribution arrangements can be specified. Minimum order quantity for custom configurations to be confirmed.
Batch production Production scheduling accommodates repeat orders for drainage fleets and rental stock. Batch sizes and production cycle times to be confirmed against current factory capacity.
Quality inspection Inspection covers engine run-in, hydraulic circuit pressure testing, relief valve verification, coupler function, and leak checks. Test records and third-party inspection arrangements to be confirmed.
Export packaging Units packed in wooden cases with hydraulic ports capped and fuel tank drained for transport. Packaging configuration for sea freight and buyer branding requirements to be confirmed.
Technical documentation Operation manual, maintenance schedule, hydraulic circuit diagram, and pump head matching record supplied with each unit. Availability of pressure test certificates and material declarations to be confirmed at inquiry stage.
B2B Buyer Considerations
Pump Head Hydraulic Matching The power unit flow and pressure must match the hydraulic motor displacement of the submersible pump heads to achieve the required impeller speed. Buyers should provide the pump head specification, including required flow, head, and hydraulic motor data, so the pump displacement and relief setting can be confirmed before shipment.
Number of Pump Heads Served Buyers planning to drive multiple submersible pump heads from one power unit should confirm the combined flow demand against the unit's rated output. Where several heads operate simultaneously, a flow divider may be required. The number of heads and their duty points should be specified at inquiry stage.
Hose Length and Routing Hoses run from the power unit to each submersible pump head, and the total hose length affects pressure loss in the circuit. Buyers should confirm the distance from the power unit position to each sump, and specify hose length accordingly. Protection at doorways, manholes, and traffic areas should be considered.
Coupler Standard and Adapters Coupler type should match the pump head connections and any existing hose inventory. Buyers with mixed pump head coupler standards should confirm whether adapters are acceptable, as adapters add potential leak points. Coupler specification can be adjusted at order stage.
Service Parts and Standby Readiness For fleet operation, buyers should hold spare filters, spark plugs, and hydraulic oil, and confirm the supplier's lead time for engine and hydraulic components. For units in standby, a defined run and inspection interval should be agreed to ensure the unit starts and delivers pressure when required.
Frequently Asked Questions

Matching requires the hydraulic motor displacement of the pump head, together with the required flow and head at the duty point. The power unit flow and pressure are then selected so the available supply produces the required impeller speed. Buyers should provide the pump head model, motor displacement, and duty point at inquiry stage. If the pump head specification is known but the hydraulic data is not, the supplier can typically match from the pump head model number.

Yes, provided the combined flow demand of the connected pump heads does not exceed the power unit's rated 35 L/min. Where several heads operate simultaneously, a flow divider may be required to maintain stable operation of each head. Buyers planning multi-point dewatering should specify the number of heads and their individual duty points so the distribution arrangement can be confirmed.

Hose length is limited by pressure loss and by the practical handling of the hose at the site. Longer hoses increase pressure loss in the circuit, which reduces the pressure available at the pump head motor. Buyers should provide the distance from the power unit position to each sump, and the supplier can confirm the appropriate hose length and any pressure compensation required. Hoses are supplied to the specified length at order stage.

The power unit can drive submersible pump heads from other manufacturers provided the hydraulic motor displacement, pressure rating, and coupler type are compatible with the unit's supply. Buyers should provide the pump head hydraulic motor specification and coupler type for confirmation. Where the coupler type differs, alternative couplers or adapters can be specified at order stage, subject to confirmation of compatibility and pressure rating.

The 6.5-litre fuel tank provides approximately 3.2 hours at rated load, depending on engine load and the number of pump heads being driven. Because the pump is pressure compensated, fuel consumption falls when pump heads operate against lower resistance or when fewer heads are connected, and runtime can extend beyond this figure. Buyers should confirm refuelling arrangements for extended pumping operations.

Check engine oil level before each use, and clean or replace the air filter according to the operating environment. Inspect hydraulic hoses and couplers for abrasion or leakage, and check the reservoir oil level. Hydraulic oil and return filter should be replaced at the interval specified in the maintenance schedule. For units in standby, run the engine briefly at defined intervals to confirm starting and hydraulic output.

A complete inquiry should include: the submersible pump head model and hydraulic motor specification; the required flow and head at each duty point; the number of pump heads to be driven and whether they operate simultaneously; the distance from the power unit to each sump and the required hose length; the coupler type used on the pump heads; and the expected duty cycle and runtime per shift. For fleet or rental procurement, indicate the estimated quantity and whether the specification must remain fixed across repeat orders.

Est. 2014 high-end hydraulic
Wuhu Qisheng
Intelligent Equipment

Professional China designer & custom manufacturer, suppliers of Hydraulic Power Unit for Submersible Pumps for emergency, rescue, agricultural water conservancy, and environmental protection.

Deeply engaged

We keep up with industry trends and empower efficient operations with professional strength.

Senior R&D engineers Technical pain point solutions Efficient production system Rapid market response
200+
projects delivered
98%
on‑time delivery
emergency rescue environmental agricultural water
Engineering excellence

Deeply engaged in the hydraulic equipment industry, we keep up with trends and empower efficient operations with professional strength. Our core competitiveness lies in strong technological and production capabilities.

We have a team of senior R&D engineers with rich practical experience. Accurately grasping technical pain points and demand directions, we provide solid support for product innovation.

Our engineers work closely with clients to translate operational challenges into precise technical specifications, ensuring every solution is fit for purpose.

Production & agility

Equipped with an efficient production system, we realize seamless connection between R&D and production, quickly respond to market changes, meet diverse customer needs, and ensure delivery efficiency and product stability.

Rapid prototyping & testing
Flexible manufacturing capacity
Just-in-time inventory management
End-to-end quality control
Lean production workflows
Automated assembly lines
24/7technical support
100+custom solutions
48hrapid response
99%quality pass rate
Product portfolio

Our products cover multiple categories including hydraulic power stations, slurry pumps, integrated and portable water pump equipment, and hydraulic breakers — for drainage, dredging, forest fire fighting, cutting, drilling, and sand suction.

With comprehensive functions, our products can be widely used in various scenarios such as drainage, dredging, forest fire fighting, cutting, drilling, and sand suction, adapting to the actual operation needs of core fields such as emergency rescue and environmental construction.

Non‑electric drive

Safe operation in hazardous environments, high lift, strong wear resistance, easy mobility — hardcore equipment under complex working conditions.

Customized R&D

Full‑process tailored solutions to solve your personalized operation problems. We design exclusive hydraulic equipment for your specific needs.

200+
projects delivered
98%
on‑time delivery
24/7
technical support
100+
custom solutions
Development philosophy
“Promoting the development of emergency rescue hydraulic equipment and leading the technological innovation of the industry.”

We adhere to the original intention of quality, focus on customers' core demands, and are committed to providing high‑quality, highly competitive products, customized solutions and comprehensive services.

Strategic partner
Reliable · professional · sustainable
Core fields
Emergency rescue Agricultural water Environmental protection Forest fire fighting
R&D driven custom solutions quality first

Get in touch