 English
 русский
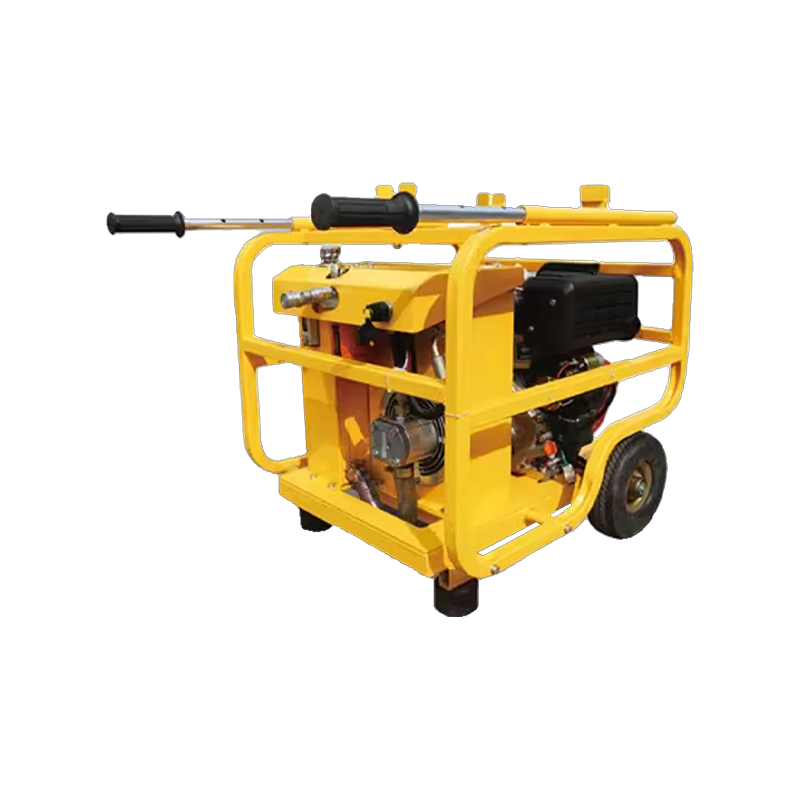

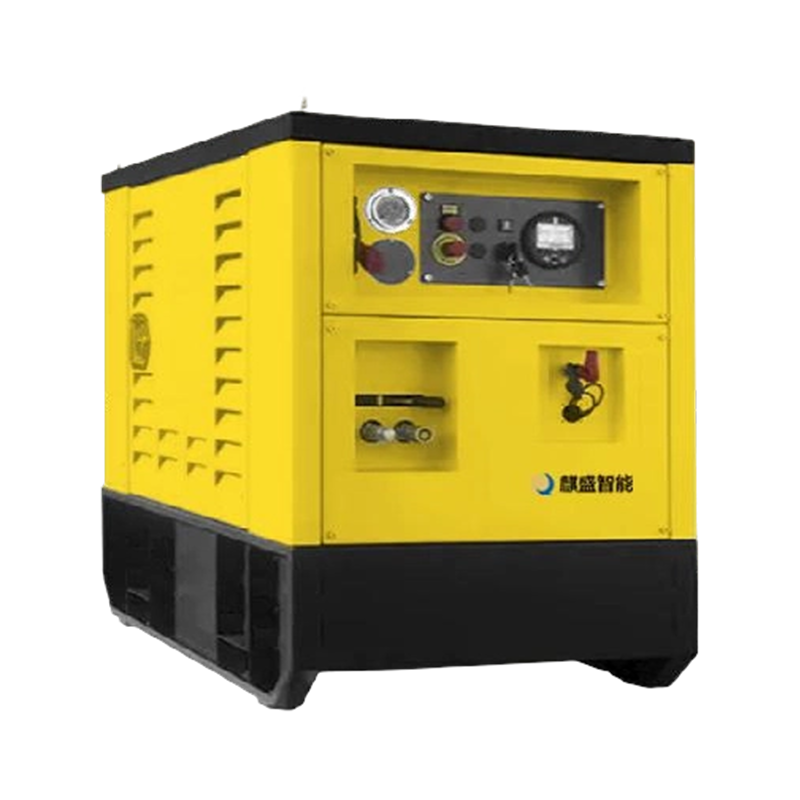
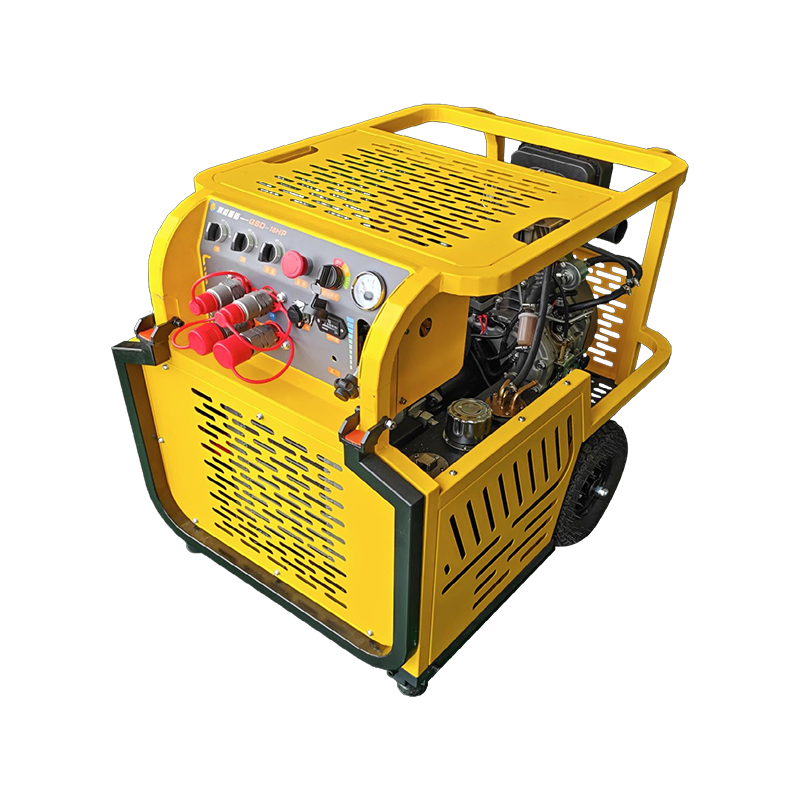
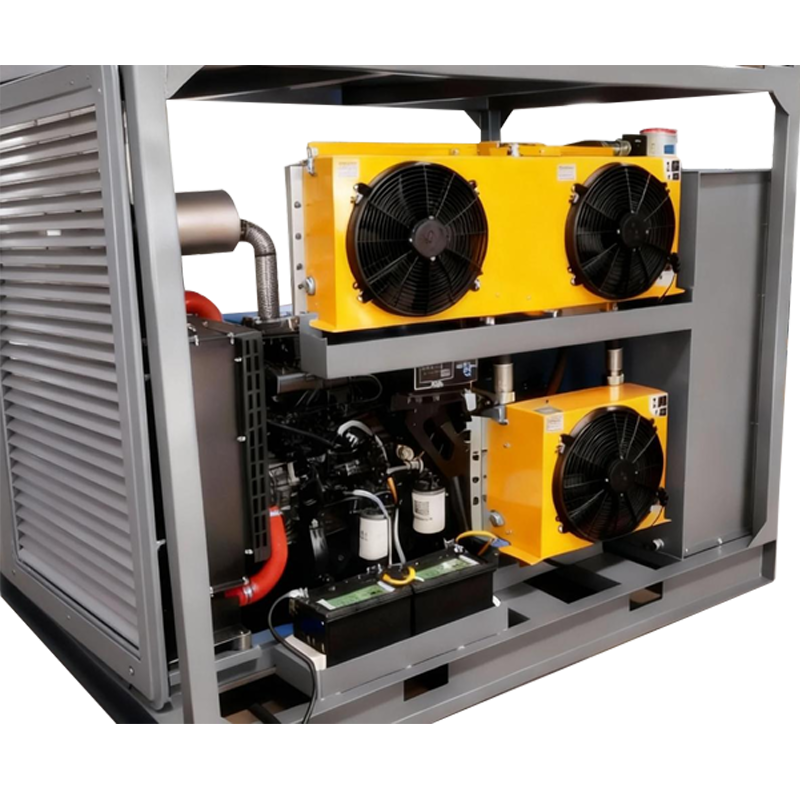
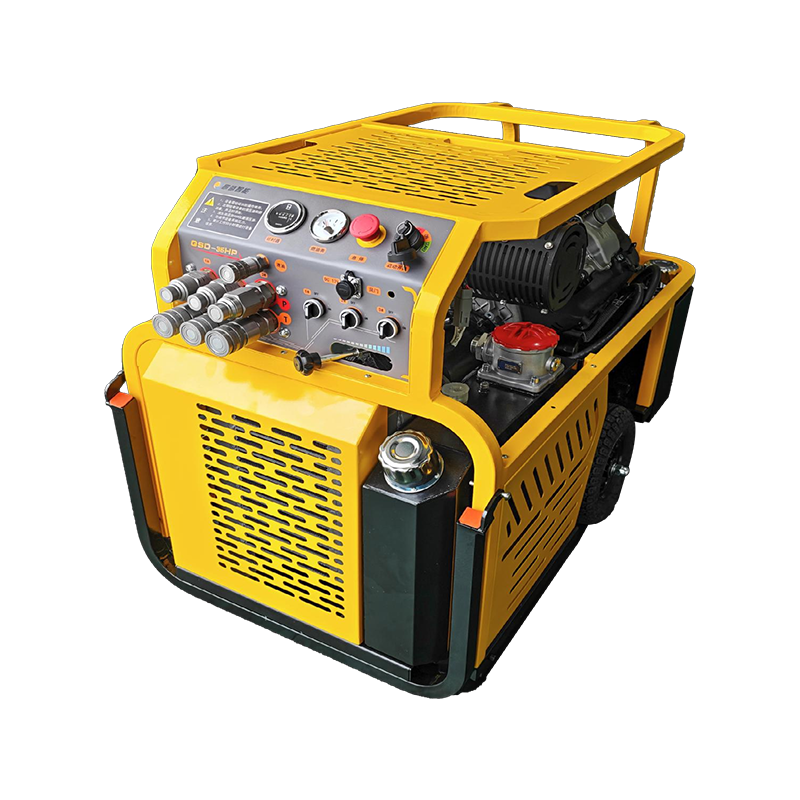
Gasoline Hydraulic Power Unit
Self-contained hydraulic power source for field service, construction, and industrial maintenance operations requiring independent prime movers
The prime mover is a 4-stroke, air-cooled gasoline engine rated at 8.0 kW continuous output. The engine features a recoil start system with automatic decompression, a low-oil shutdown sensor, and a centrifugal governor for stable speed control. A 5.5-liter fuel tank provides approximately 4 hours of operation at rated load. The engine is mounted on anti-vibration isolators to reduce transmission of vibration to the hydraulic circuit and frame.
The hydraulic system uses a variable-displacement axial piston pump with pressure compensation, delivering up to 32 L/min at 210 bar. The pump automatically adjusts displacement based on downstream pressure, reducing heat generation and fuel consumption when tools are idle. The 14-liter reservoir incorporates a 10-micron return filter with bypass indicator, a magnetic drain plug, and a sealed breather. A thermostatically controlled air-oil cooler maintains fluid temperature within the optimal range.
The unit is mounted on a heavy-gauge steel skid with integrated lifting eyes and forklift pockets for mechanical handling. Two 200 mm wheels and a foldable handle enable single-operator transport across job sites. The frame includes a drip tray to contain minor hydraulic leaks and protect the environment. A protective roll bar shields the engine and pump from impact damage during transport and operation.
The unit provides two sets of ISO 16028 flat-face quick couplers rated for 250 bar, enabling connection of two tools or circuits simultaneously. A panel-mounted pressure gauge allows visual monitoring of system pressure. A manual pressure relief valve protects the circuit from overpressure. All hydraulic lines are rated for 250 bar working pressure with a 4:1 safety factor.
At 100 percent rated load (32 L/min at 210 bar), the 5.5-liter fuel tank provides approximately 3.5 hours of continuous operation. At typical field usage with intermittent tool demand, runtime extends to 5-6 hours. The pressure-compensated pump reduces fuel consumption during idle periods, which further extends operational time between refueling.
The unit is equipped with two sets of ISO 16028 couplers, enabling simultaneous connection of two tools or circuits. However, the total combined flow demand must not exceed 32 L/min. If both tools require full flow simultaneously, a flow divider is recommended to ensure stable operation of both circuits.
ISO VG 46 mineral hydraulic oil is specified for operation in ambient temperatures from 10°C to 45°C. For operation below 10°C, ISO VG 32 is recommended. For operation above 45°C, ISO VG 68 may be used. The unit is supplied with ISO VG 46 factory fill. Oil change interval is 200 hours or 12 months, whichever occurs first.
The unit is designed for outdoor use and requires adequate ventilation when operated indoors. Gasoline engines produce carbon monoxide and must never be operated in enclosed spaces without proper exhaust extraction. For indoor applications, an exhaust extension kit is available to route emissions to a safe location. Alternatively, an electric-driven version of this unit is available for indoor use.
Each unit is supplied with an operation and maintenance manual, a commissioning checklist, a parts catalog, and a CE declaration of conformity. For fleet procurement, technical datasheets and CAD models are available upon request. Spare parts lists include recommended spares for 2000-hour and 5000-hour service intervals.