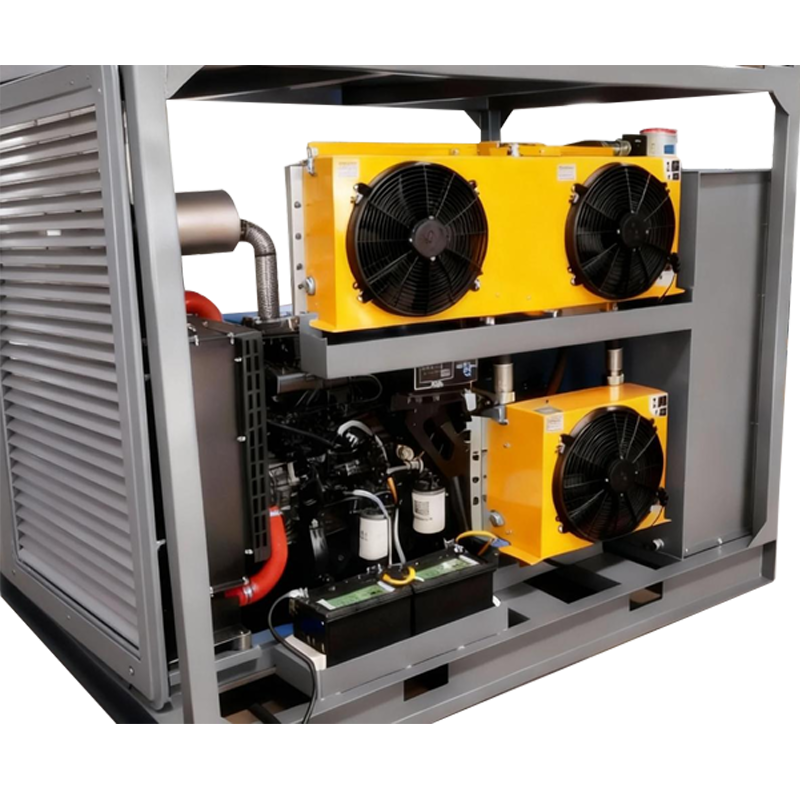
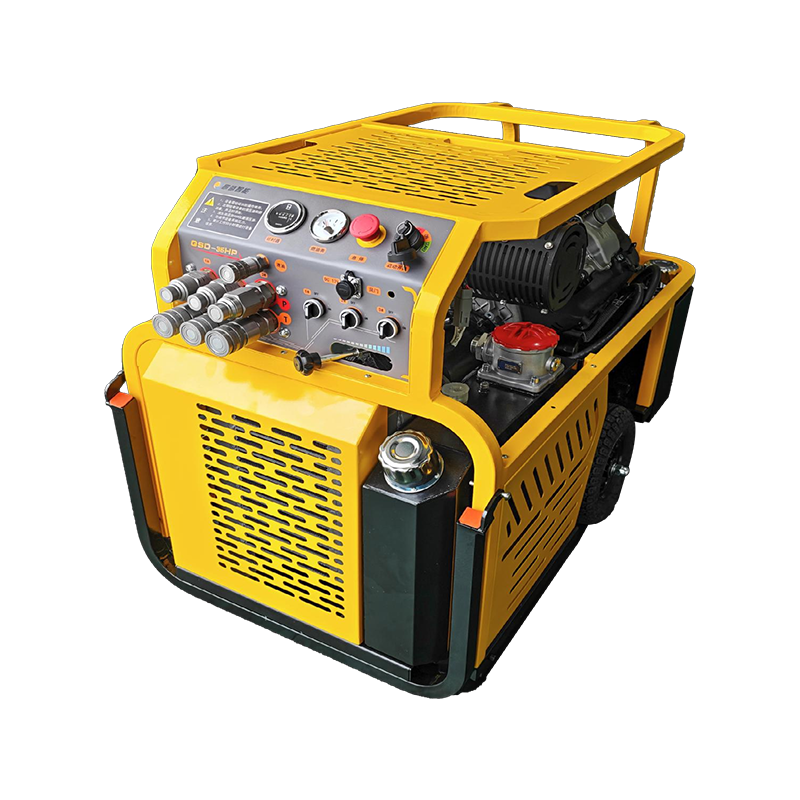
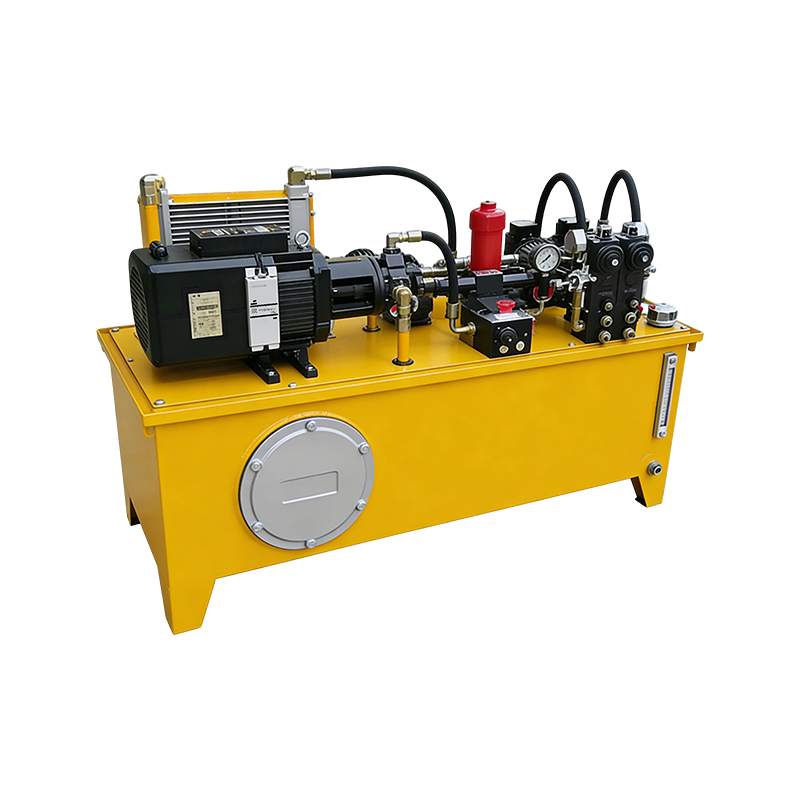
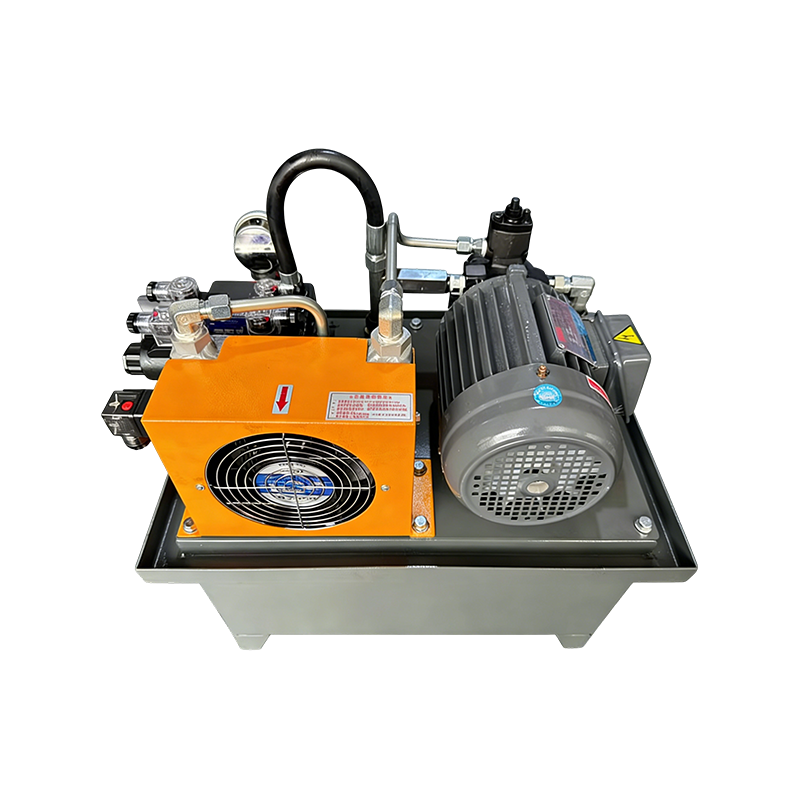
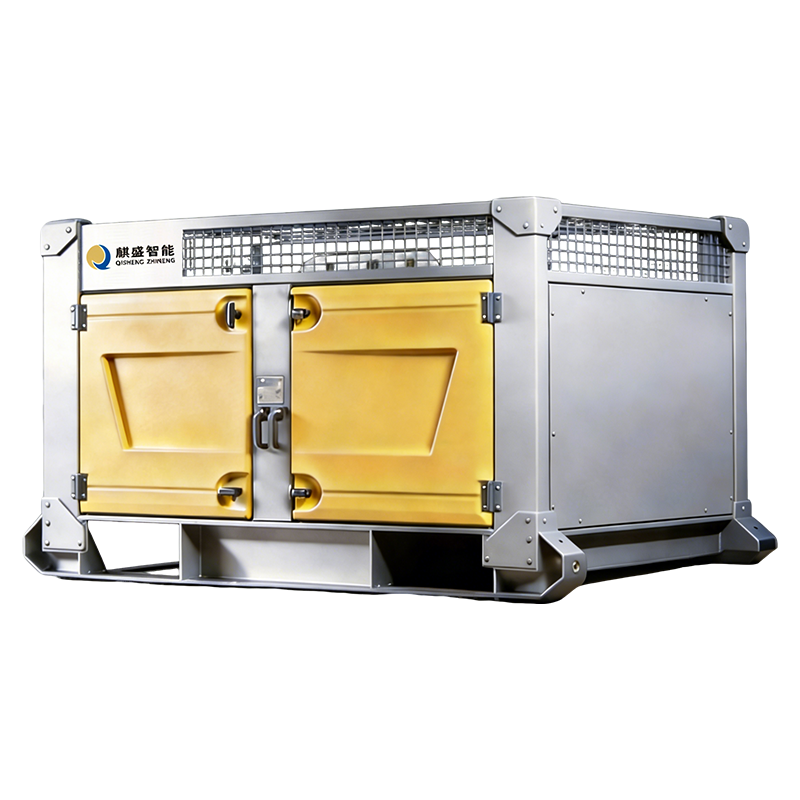
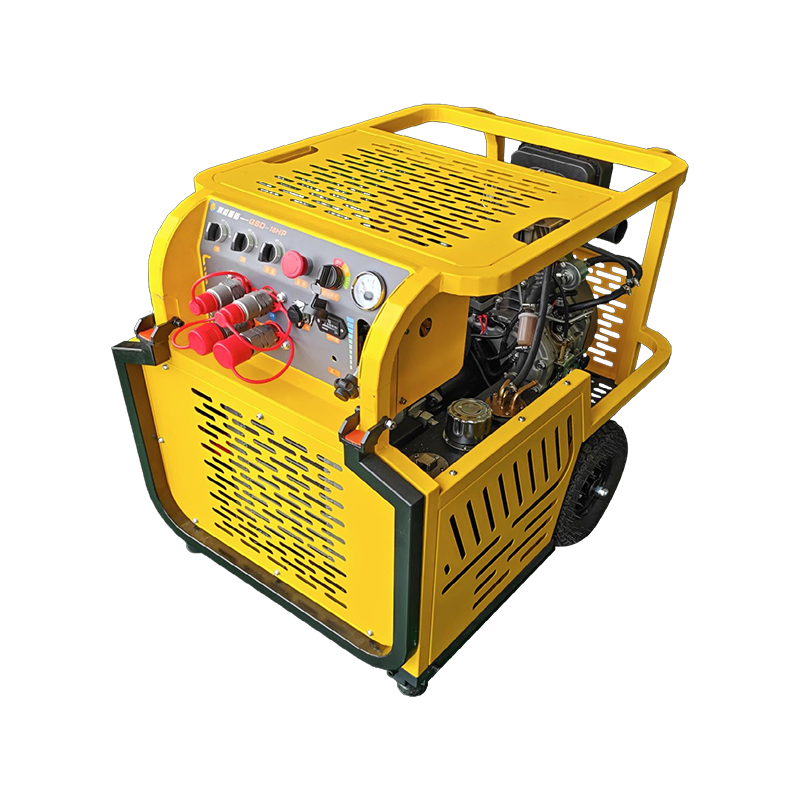
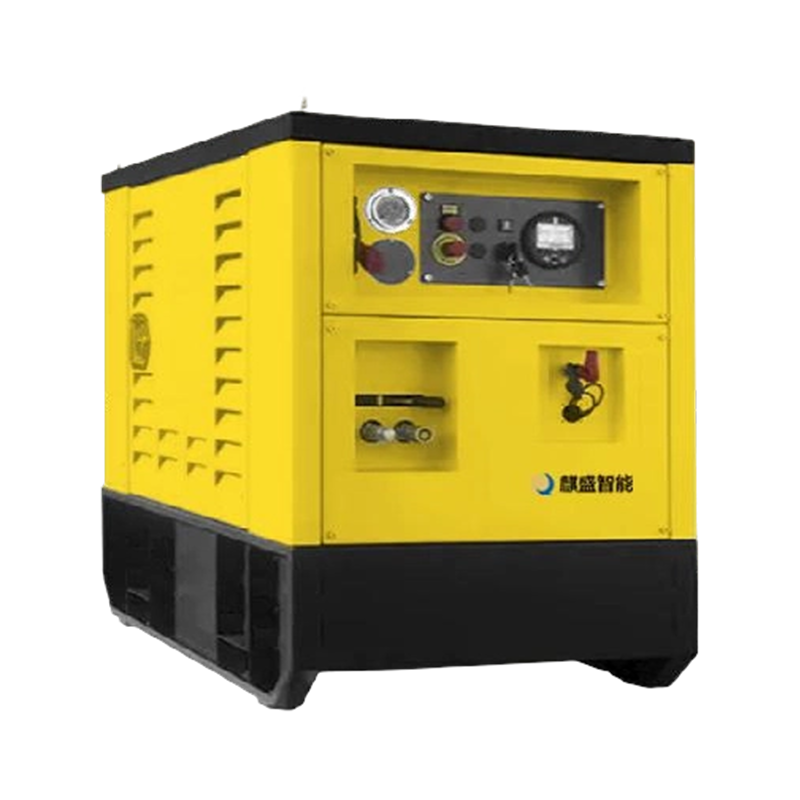
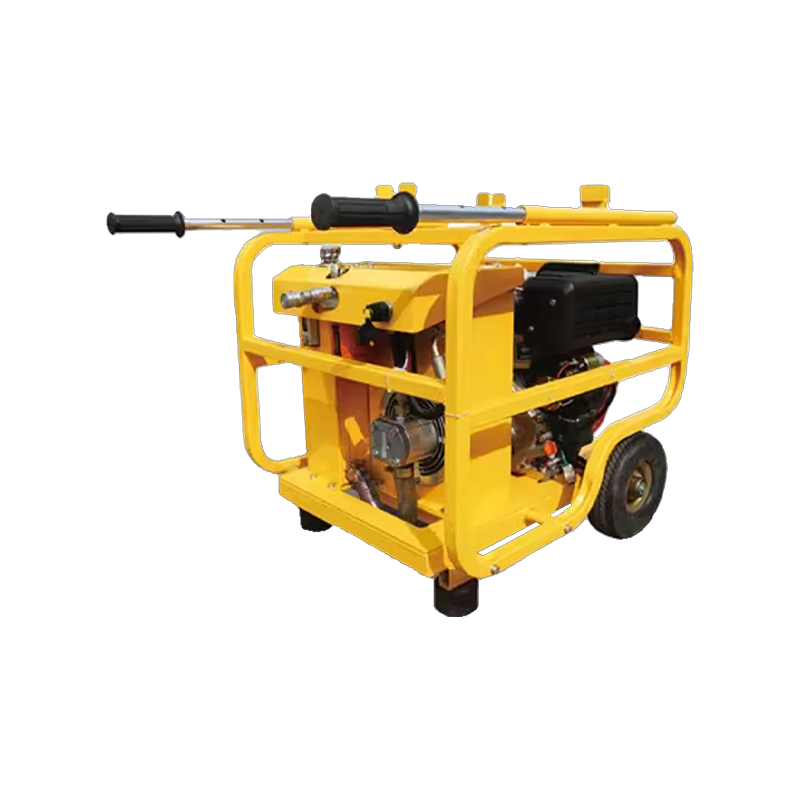
Skid-Mounted Configuration
Equipment Datasheet Rev. 4.2

Diesel Driven Hydraulic Power Unit

A continuous-duty hydraulic power source engineered for heavy industrial, mining, and construction applications where electrical supply is unavailable or unreliable. The unit integrates a water-cooled diesel engine with a load-sensing axial piston pump, delivering stable flow and pressure for high-demand hydraulic circuits. Designed for unattended operation, remote deployment, and integration with mobile machinery and fixed plant equipment.

90 L/min Max Flow
250 bar Max Pressure
22.5 kW Engine Output
120 L Reservoir
Engine and Drive System

The prime mover is a water-cooled, four-cylinder diesel engine rated at 22.5 kW continuous output. The engine is equipped with a mechanical governor, electric start, and a 45-liter fuel tank providing approximately 10 hours of operation at 75 percent load. An integrated radiator with hydraulic fan drive maintains stable operating temperature in ambient conditions up to 50°C. The engine couples directly to the pump through a bell housing and flexible coupling, eliminating belt drive maintenance and alignment issues. A dual-stage air filter with restriction indicator protects the engine in dusty environments.

Engine type 4-cylinder, water-cooled diesel
Continuous output 22.5 kW (30 HP) at 2200 rpm
Fuel consumption 4.8 L/h at 75% load
Fuel tank 45 L
Starting system 12V electric start, 80Ah battery
Cooling Integrated radiator, hydraulic fan
Air filtration Dual-stage with restriction indicator
Hydraulic Circuit

The hydraulic system employs a variable-displacement axial piston pump with load-sensing control, delivering up to 90 L/min at 250 bar working pressure. The load-sensing regulator adjusts pump displacement based on downstream demand, reducing heat generation and fuel consumption during idle or low-flow periods. The 120-liter reservoir incorporates a 10-micron full-flow return filter with bypass indicator, a magnetic drain plug, and an air breather with desiccant. A thermostatically controlled oil cooler maintains reservoir temperature within the optimal 45-60°C range. The circuit includes a main pressure relief valve, a pressure gauge, and two sets of ISO 16028 flat-face couplers for tool connection.

Pump type Variable axial piston, load-sensing
Maximum flow 90 L/min
Maximum pressure 250 bar
Reservoir capacity 120 L
Filtration 10 micron absolute, full-flow
Oil cooling Thermostatic, air-oil cooler
Couplers ISO 16028 flat-face, 2 sets
General Specifications Skid-mounted configuration
Dimensions (L x W x H) 1450 x 820 x 1050 mm
Dry weight 480 kg
Operating weight 620 kg (with full fuel and oil)
Skid material Heavy-gauge steel with anti-corrosion coating
Handling provisions 4 lifting eyes, 2 forklift pockets
Noise level 78 dB(A) at 1 m
Ambient temperature range -15°C to 50°C
Emissions compliance EU Stage V, EPA Tier 4 Final
Industrial Applications
Mobile crushing and screening plants
Mining equipment and drilling rigs
Heavy lifting and jacking systems
Pipeline construction equipment
Offshore and marine deck machinery
Emergency power for hydraulic gates
Control and Monitoring
C1 Local control panel with pressure gauge and flow indicator
C2 Engine protection shutdown for low oil pressure and high coolant temperature
C3 Hour meter and service interval indicator
C4 Optional CAN bus telemetry for remote monitoring
C5 Fuel level sensor with low-fuel alarm output
C6 Emergency stop with manual reset
Service and Supply
Standard supply Power unit, operation manual, commissioning checklist
Optional equipment Telemetry module, cold-weather package, extended hose sets
Oil change interval 500 hours or 12 months
Filter change interval 500 hours
Warranty 24 months or 2000 hours
Technical support Regional service network, 48-hour response
Technical and Procurement Clarifications

Fuel consumption depends on load profile. At 75 percent continuous load, consumption is approximately 4.8 liters per hour. At idle or low-flow demand, the load-sensing pump reduces engine load and consumption drops to approximately 1.8 liters per hour. The 45-liter tank provides approximately 10 hours of operation at 75 percent load or up to 24 hours under light intermittent demand.

The standard configuration operates from -15°C to 50°C with appropriate hydraulic oil selection. For sustained operation below -15°C, a cold-weather package is available that includes engine block heater, battery warming blanket, arctic-grade hydraulic oil, and heated control enclosure. This package extends the operating range to -30°C.

The unit is supplied with two sets of ISO 16028 flat-face couplers rated for 250 bar. Connection to existing machinery requires matching couplers on the machine side. For machines with different connection standards, adapter sets are available. The load-sensing pump automatically adjusts to the flow and pressure requirements of the connected circuit, simplifying integration.

Engine oil and filter change: every 250 hours. Fuel filter: every 500 hours. Air filter: inspected every 100 hours, replaced when restriction indicator activates. Coolant: checked weekly, replaced every 2000 hours or 24 months. Valve clearance: adjusted every 1000 hours. The unit includes a service interval indicator on the control panel.

Yes. An optional CAN bus telemetry module enables remote monitoring of engine parameters, hydraulic pressure and flow, fuel level, and fault codes. Data are transmitted via 4G LTE or satellite depending on site coverage. The system supports integration with SCADA platforms through Modbus TCP and can generate SMS or email alerts for critical events.

Est. 2014 high-end hydraulic
Wuhu Qisheng
Intelligent Equipment

Professional China designer & custom manufacturer, suppliers of Diesel Driven Hydraulic Power Unit for emergency, rescue, agricultural water conservancy, and environmental protection.

Deeply engaged

We keep up with industry trends and empower efficient operations with professional strength.

Senior R&D engineers Technical pain point solutions Efficient production system Rapid market response
200+
projects delivered
98%
on‑time delivery
emergency rescue environmental agricultural water
Engineering excellence

Deeply engaged in the hydraulic equipment industry, we keep up with trends and empower efficient operations with professional strength. Our core competitiveness lies in strong technological and production capabilities.

We have a team of senior R&D engineers with rich practical experience. Accurately grasping technical pain points and demand directions, we provide solid support for product innovation.

Our engineers work closely with clients to translate operational challenges into precise technical specifications, ensuring every solution is fit for purpose.

Production & agility

Equipped with an efficient production system, we realize seamless connection between R&D and production, quickly respond to market changes, meet diverse customer needs, and ensure delivery efficiency and product stability.

Rapid prototyping & testing
Flexible manufacturing capacity
Just-in-time inventory management
End-to-end quality control
Lean production workflows
Automated assembly lines
24/7technical support
100+custom solutions
48hrapid response
99%quality pass rate
Product portfolio

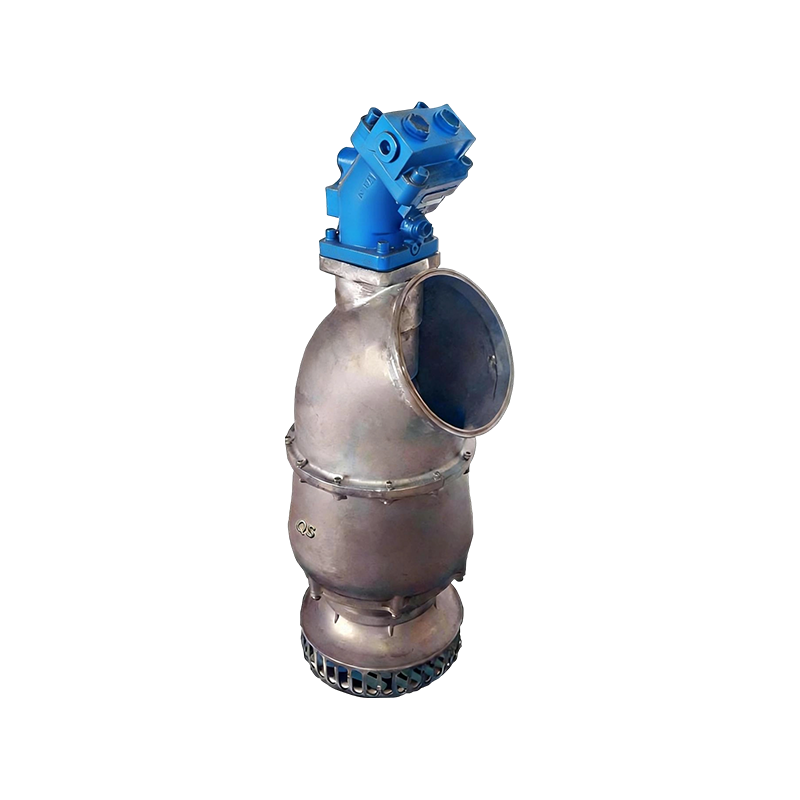
Our products cover multiple categories including hydraulic power stations, slurry pumps, integrated and portable water pump equipment, and hydraulic breakers — for drainage, dredging, forest fire fighting, cutting, drilling, and sand suction.

With comprehensive functions, our products can be widely used in various scenarios such as drainage, dredging, forest fire fighting, cutting, drilling, and sand suction, adapting to the actual operation needs of core fields such as emergency rescue and environmental construction.

Non‑electric drive

Safe operation in hazardous environments, high lift, strong wear resistance, easy mobility — hardcore equipment under complex working conditions.

Customized R&D

Full‑process tailored solutions to solve your personalized operation problems. We design exclusive hydraulic equipment for your specific needs.

200+
projects delivered
98%
on‑time delivery
24/7
technical support
100+
custom solutions
Development philosophy
“Promoting the development of emergency rescue hydraulic equipment and leading the technological innovation of the industry.”

We adhere to the original intention of quality, focus on customers' core demands, and are committed to providing high‑quality, highly competitive products, customized solutions and comprehensive services.

Strategic partner
Reliable · professional · sustainable
Core fields
Emergency rescue Agricultural water Environmental protection Forest fire fighting
R&D driven custom solutions quality first

Get in touch