English
 русский
Qisheng
Qisheng
Qisheng
Qisheng
Qisheng
Qisheng
Qisheng
Qisheng
Qisheng
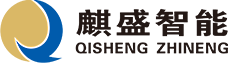


Drain outlet diameter 75mm, 2030Lpm Submersible Hydraulic Slurry Pump
Product Model: QSZB1203580
The QSZB1203580 Hydraulic Slurry Pump is hydraulically driven and features a pump body constructed from stainless steel casting and an impeller made of cast iron, offering excellent wear and corrosion resistance. The equipment incorporates a special vortex flow channel design, allowing the passage of large solid particles up to 60100mm and enabling the handling of high-concentration media. It operates at a working pressure of 140 bar, delivers a flow rate of up to 120 m³/h, and provides a head of 35 meters. The product has a total weight of 25 kg and compact dimensions (320×370×440mm), requiring a hydraulic flow of 2035 Lpm. This pump is suitable for transporting slurries containing solid particles, pulp, viscous fluids, and municipal sewage, meeting the requirements for drainage and dredging operations under complex working conditions.
- Product Details
- About Qisheng
- Contact Us
QSZB SERIES
75mm Submersible Hydraulic Slurry Pump
2030 Lpm Max Flow
140 Bar Pressure
75 mm Outlet
The QSZB series submersible hydraulic slurry pump is engineered for continuous operation in high-solids and abrasive environments. Driven by an external hydraulic power source, it eliminates the risk of electrical failure during submerged use. The 75mm outlet configuration (QSZB120-35-80) delivers a maximum flow rate of 120 m³/h (approx. 2000 Lpm) and a head of 35 meters, making it suitable for heavy-duty dewatering in mining, tunneling, and municipal emergency response. Its cast-iron open impeller and dual-lip seal ensure reliable performance in challenging slurry conditions.
Technical Performance & Configuration
Hydraulic Drive System
Requires external power unit (20-35 Lpm flow at 140 bar). No internal electrical components, ensuring safe operation in flooded or explosive environments.
High-Solids Handling
The open impeller design and cast-iron volute allow the passage of solid particles up to 25mm. Ideal for abrasive slurry and debris-laden water.
Seal Protection
Dual-lip mechanical seal in an oil bath prevents abrasive materials from entering the bearing chamber, extending the service life of the drive shaft.
Portability & Installation
Weight of 25kg and compact dimensions (320×370×440 mm) allow for manual positioning. Standard quick couplers connect the pump to the hydraulic circuit in seconds.
Model Matrix
All specifications are subject to standard manufacturing tolerances.| Model | Drain Outlet (mm) | Max Flow (m³/h) | Max Head (m) | Working Pressure (bar) | Weight (kg) | Flow Range (Lpm) | Dimensions (mm) |
| QSZB100-40-50 | 50 | 100 | 40 | 140 | 13 | 20-30 | 320*220*430 |
| QSZB120-35-80 | 75 | 120 | 35 | 140 | 25 | 20-35 | 320*370*440 |
| QSZB200-25-100 | 100 | 200 | 25 | 150 | 29 | 30-40 | 346*268*510 |
| QSZB280-25-150 | 150 | 280 | 25 | 160 | 38 | 50-72 | 460*320*520 |
Engineering Notes
The open impeller design allows solid particles up to 25mm in diameter to pass through without clogging. For larger debris, a strainer is recommended at the suction inlet.
Hydraulic drive eliminates the need for electrical components in the sump, reducing the risk of short circuits and allowing operation in deeper or more hazardous environments. It also provides variable speed control via the power pack.
The oil bath should be checked periodically for contamination. If slurry is detected in the oil, the seal should be replaced. Regular inspection extends the life of the bearing chamber.
ISO VG 46 hydraulic oil filtered to ISO 18/16/13 is recommended. Contaminated oil can accelerate wear on the internal gear motor and reduce seal life. Regular oil sampling is advised in high-particulate environments.
The pump should not be operated dry for extended periods. While the hydraulic motor is independent of the slurry, the mechanical seal relies on the pumped liquid for cooling and lubrication. Short dry runs during positioning are acceptable.
Deployment Fields
- Mining Operations: Sump cleaning and transfer of abrasive tailings.
- Tunnel Construction: Removal of drill water and fine rock slurry.
- Flood Emergency: Rapid dewatering of basements and underpasses.
- Industrial Pits: Process water transfer with high solid content.
Wuhu Qisheng Intelligent Equipment Co., Ltd. is a professional designer and manufacturer of high-end hydraulic equipment focusing on emergency, rescue, agricultural water conservancy, environmental protection and other fields. Deeply engaged in the hydraulic equipment industry, we keep up with the industry development trend and empower efficient operations in various fields with professional strength to promote high-quality industrial development. The company's core competitiveness lies in its strong technological and production capabilities. We have a team of senior professional R&D engineers, all of whom have rich practical experience in industry development. Deeply rooted in the R&D field of hydraulic equipment, they accurately grasp the industry's technical pain points and demand directions, providing solid support for product innovation and upgrading. At the same time, the company is equipped with an efficient production system, realizing the efficient connection between R&D and production, which can quickly respond to market changes, timely meet the diverse needs of different customers, and ensure delivery efficiency and product stability.
In terms of product layout, the company focuses on the core field of emergency rescue hydraulic equipment. The developed products cover multiple categories such as hydraulic power stations, slurry pumps, integrated and portable water pump equipment, and hydraulic breakers. With comprehensive functions, the products can be widely used in various scenarios such as drainage, dredging, forest fire fighting, cutting, drilling, and sand suction, adapting to the actual operation needs of core fields such as emergency rescue and environmental construction. With the advantages of non-electric drive, high lift, strong wear resistance and easy mobility, they have become "hardcore equipment" under complex working conditions. Relying on strong design and development capabilities, the company not only provides high-quality standardized products, but also deeply understands customers' specific working condition needs, provides full-process customized R&D solutions, and tailors exclusive hydraulic equipment to effectively solve customers' personalized operation problems.
Upholding the development philosophy of "promoting the development of emergency rescue hydraulic equipment and leading the technological innovation of the industry", the company always adheres to the original intention of quality, focuses on customers' core demands, and is committed to providing customers with high-quality, highly competitive products, customized solutions and comprehensive services. With reliable product performance and professional service guarantee, we create sustainable value for customers, deeply cultivate the industry, forge ahead steadily, and strive to become a trusted strategic partner of customers in the high-end hydraulic equipment field.
Hot Products
-


Drain outlet diameter 50mm, 2030Lpm Submersible Hydraulic Slurry Pump
-

Drain outlet diameter 150mm, 5072Lpm Submersible Hydraulic Slurry Pump
-
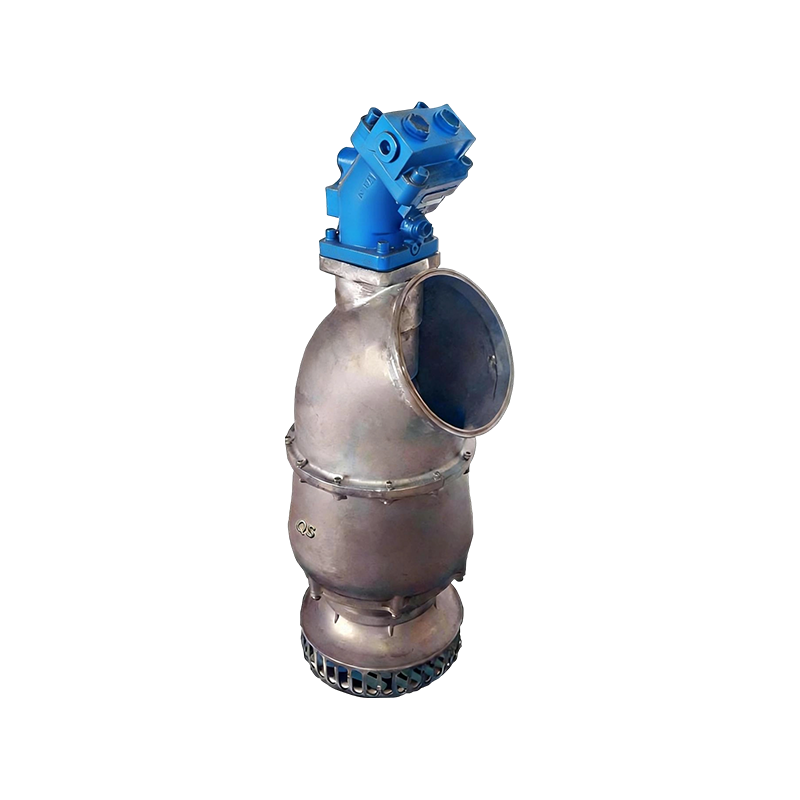
Hydraulic Driven Axial Flow Flood Pump (12inch)
-
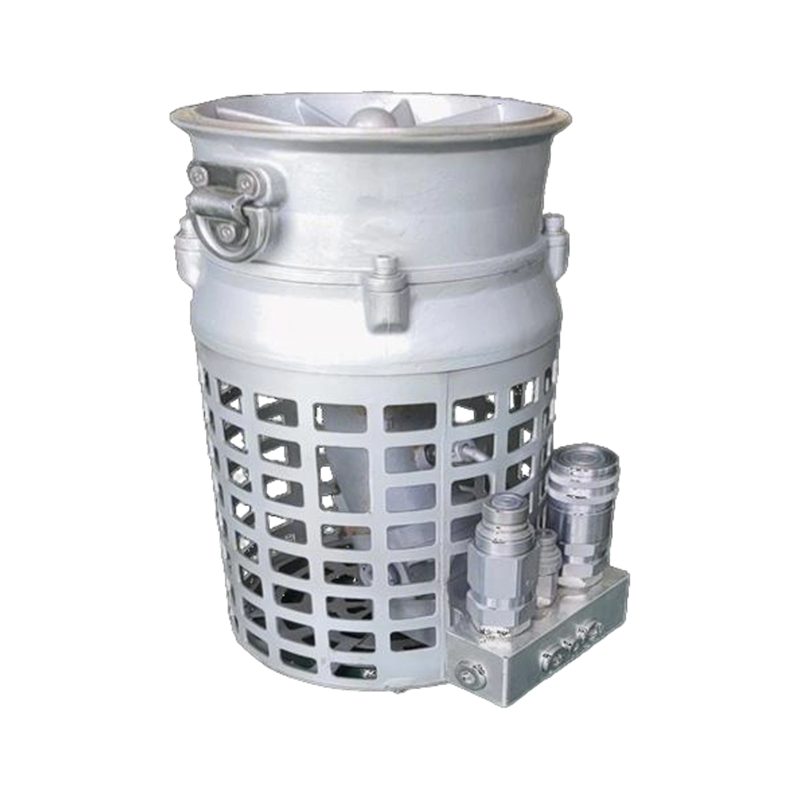
8inch HighFlow Hydraulic Submersible Axial Pump
-
8inch HighFlow Hydraulic Axial Flow Pump
-
Stainless Steel HighFlow Electric Drainage Pumps (4inch-14inch)
About Qisheng
Wuhu Qisheng Intelligent Equipment Co., Ltd.
Wuhu Qisheng Intelligent Equipment Co., Ltd. is a professional designer and manufacturer of high-end hydraulic equipment for emergency, rescue, agriculture, and environmental protection. Our core competitiveness lies in a senior R&D team with deep industry expertise and an efficient production system that ensures rapid market response and product stability.
We are China Drain outlet diameter 75mm, 2030Lpm Submersible Hydraulic Slurry Pump Suppliers and Wholesale Drain outlet diameter 75mm, 2030Lpm Submersible Hydraulic Slurry Pump Exporter, Company.
Focusing on emergency rescue, our product range includes hydraulic power stations, slurry pumps, portable water pumps, and breakers. These "hardcore" tools feature non-electric drive, high lift, and wear resistance, making them ideal for drainage, dredging, and forest firefighting. Beyond standardized products, we provide full-process customized R&D solutions to solve specific operational challenges.
Upholding the philosophy of leading technological innovation, we prioritize quality and customer demands. We are committed to delivering high-performance products and professional services, striving to be a trusted strategic partner in the high-end hydraulic equipment field.
Certificate Of Honor
Latest Updates
-

 Industry News
 2026.11.06
Two hydraulic breakers leave the depot behind the same 35 HP power pack. One hammers at its rated blow rate for a full shift. The other stalls at roughly 1,100 blows per minute, runs hot, and darkens the return filter inside three hours. The breaker is the s...
-
Industry News
2026.11.04
At 04:10 a municipal crew reaches a flooded underpass holding 1.4 metres of standing water. The truck-mounted set they brought needs a suction line, a priming cycle and a dry, stable power feed at the rim before a single litre moves. The hydraulic drainage r...
-
Industry News
2026.10.30
A drainage operation at an industrial plant rarely fails because the pump lacks power. It fails because the pump cannot reach the water, cannot be positioned safely, or cannot keep running on unstable ground. Drainage robots for industrial water management ca...
Drain outlet diameter 75mm, 2030Lpm Submersible Hydraulic Slurry Pump Industry knowledge
What Key Features Should You Look for in a Submersible Hydraulic Slurry Pump?
A modern submersible hydraulic slurry pump is engineered to handle abrasive, high-density mixtures in challenging environments where conventional pumping systems often struggle. Selecting the right unit requires a clear understanding of hydraulic efficiency, wear resistance, flow capacity, structural durability, and system compatibility.
Core Function and Working Principle
A submersible hydraulic slurry pump operates by converting hydraulic energy into mechanical pumping force, allowing the unit to function fully submerged in slurry media. Unlike electric-driven systems, hydraulic-driven designs provide higher torque stability and improved resistance to overload conditions.
Key functional expectations include:
- Continuous handling of abrasive slurry mixtures
- Stable performance under variable density conditions
- Efficient heat dissipation through surrounding fluid
- Reduced risk of cavitation in deep or confined environments
These characteristics make it suitable for mining, dredging, emergency drainage, and environmental sediment removal tasks.
Key Performance Features to Evaluate
When selecting a pump, several technical attributes define overall performance and suitability:
- Hydraulic power efficiency
- Solid particle handling capability
- Wear-resistant structure design
- Flow stability under pressure fluctuation
- Operational depth adaptability
Feature Comparison Table
| Feature Category | Performance Requirement | Operational Benefit |
|---|---|---|
| Hydraulic Efficiency | High torque output, low energy loss | Stable long-term operation |
| Solid Handling Ability | Large particle tolerance | Reduced clogging risk |
| Structural Design | Reinforced casing | Extended service life |
| Cooling Method | Submersion-based cooling | No overheating issues |
| Flow Stability | Consistent output under load | Reliable pumping performance |
Hydraulic System Compatibility
Compatibility with hydraulic power units is a critical selection factor. A well-matched system ensures efficient energy transfer and stable flow delivery. Poor compatibility can lead to reduced output and excessive mechanical wear.
A company such as Wuhu Qisheng Intelligent Equipment Co., Ltd. focuses on optimizing hydraulic integration through advanced R&D capabilities. Their engineering teams emphasize system-level matching to ensure pumps maintain efficiency across varying working conditions.
Important considerations include:
- Hydraulic pressure range matching
- Flow regulation stability
- Hose and coupling compatibility
- Anti-leak and sealing integrity
Material Selection and Wear Resistance
Since slurry media often contains abrasive solids, material selection is one of the most important determinants of pump lifespan.
Material Performance Comparison
| Component Area | Common Material Options | Performance Characteristics |
|---|---|---|
| Impeller | High-chrome alloy steel | Excellent abrasion resistance |
| Pump casing | Hardened cast iron | Strong structural durability |
| Shaft | Alloy steel with treatment | High torsional strength |
| Seals | Mechanical seal composites | Leakage prevention under pressure |
A well-optimized material structure ensures the pump can operate continuously in harsh slurry conditions without frequent maintenance interruptions.
Flow Capacity and High-Output Performance
For large-scale operations, flow capacity becomes a defining factor. High-performance models such as the 2030Lpm submersible hydraulic slurry pump are designed for rapid material transfer and efficient sediment displacement.
High-flow system advantages include:
- Faster dredging cycles
- Improved productivity in large-scale projects
- Reduced operational downtime
- Enhanced adaptability to variable slurry concentrations
Flow optimization is closely linked to impeller design, hydraulic input stability, and discharge channel geometry. Balanced integration of these elements ensures smooth output without excessive vibration or turbulence.
Operational Efficiency and System Reliability
Operational efficiency is not only about flow rate but also about long-term stability and maintenance frequency. A well-designed hydraulic slurry pump should maintain performance consistency over extended duty cycles.
Key efficiency factors:
- Reduced internal energy loss
- Anti-clogging hydraulic pathways
- Modular structure for easy maintenance
- Stable pressure distribution system
Another important contributor is intelligent manufacturing and production control. Wuhu Qisheng Intelligent Equipment Co., Ltd. integrates advanced production systems with R&D to ensure that design improvements translate directly into reliable manufacturing quality and consistent field performance.
Application Suitability Overview
A submersible hydraulic slurry pump must be adaptable to multiple working environments. Its structural flexibility determines how effectively it can be deployed across industries.
Application Suitability Table
| Application Area | Operational Role | Required Pump Feature |
|---|---|---|
| Mining operations | Ore slurry transfer | High wear resistance |
| Environmental dredging | Sediment removal | High flow capacity |
| Emergency drainage | Flood water and debris discharge | Fast deployment ability |
| Agricultural water use | Canal cleaning and irrigation support | Stable low-pressure flow |
This versatility makes hydraulic slurry pumps a core solution in both industrial and environmental systems.
Engineering Strength and R&D Capability
Continuous innovation is essential for improving slurry pump performance. Strong engineering teams enable better adaptation to evolving industrial demands.
Wuhu Qisheng Intelligent Equipment Co., Ltd. maintains a dedicated R&D structure focused on hydraulic optimization, structural enhancement, and real-world application testing. Their engineering approach emphasizes:
- Rapid adaptation to market requirements
- Continuous hydraulic performance improvement
- Integration of advanced manufacturing techniques
This ensures that each generation of pump achieves higher efficiency and operational stability.
Conclusion
Selecting a submersible hydraulic slurry pump requires a systematic evaluation of hydraulic efficiency, material durability, flow capacity, and system compatibility. High-performance models such as the 2030Lpm submersible hydraulic slurry pump demonstrate how advanced engineering can significantly improve operational efficiency in demanding environments. By focusing on structural strength, hydraulic optimization, and application adaptability, users can ensure long-term reliability and reduced operational costs.
FAQ
1. What is the main advantage of a submersible hydraulic slurry pump?
It provides high torque performance and stable operation in abrasive and high-density slurry environments.
2. Why is flow capacity important in slurry pumping systems?
Higher flow capacity improves material transfer efficiency and reduces operational cycle time.
3. What materials are commonly used for wear resistance?
High-chrome alloys, hardened cast iron, and treated alloy steels are commonly used for durability.
4. Can hydraulic slurry pumps operate continuously underwater?
Yes, they are designed for full submersion with hydraulic-driven cooling and stable operation.
5. What factors affect pump efficiency the most?
Hydraulic system matching, impeller design, material selection, and flow stability are key factors.
Contact us
-

-

+ 86 - 553 7652 528
-

Shengqiao Street, Jiafa Town, Nanling County, Wuhu City, Anhui Province, China